The investment casting process, step by step.
From the wax replica of the component to molten metal pouring, machining and final inspection: nine steps to produce complex, accurate and repeatable parts.
Three main stages, one complete manufacturing process
Investment casting, also known as lost wax casting, uses a wax pattern that reproduces the component while compensating for shrinkage during the process.
The pattern is enclosed in a ceramic shell. Once the wax has been removed, molten metal fills the empty cavity and takes the shape of the required component.
Wax tree production
Wax pattern injection and assembly onto the central sprue.
Ceramic shell preparation
Successive ceramic coatings, dewaxing and high-temperature firing.
Component production
Metal pouring, shell removal, finishing, machining and final inspection.
The nine steps of investment casting
Every stage affects dimensional accuracy, surface quality and the metallurgical integrity of the casting.
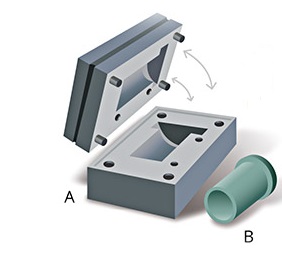
Wax pattern injection
Wax is injected into dedicated tooling to produce patterns matching the geometry of the final component. This stage determines the accuracy, repeatability and quality of the part.
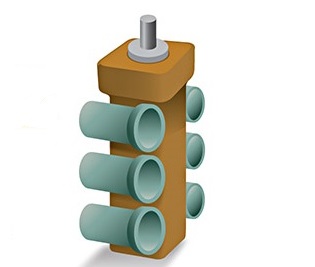
Wax tree assembly
The wax patterns are attached to a central wax sprue by controlled heating, creating a single structure commonly called a wax tree.
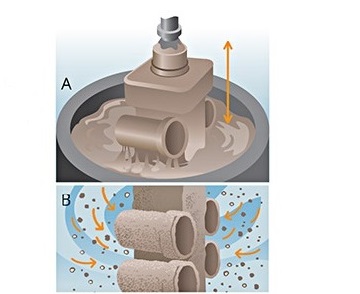
Ceramic shell production
The wax tree is repeatedly dipped into ceramic slurry and coated with refractory material. The first layer, which is in direct contact with the wax, is critical to the final surface quality.
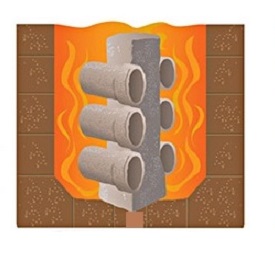
Dewaxing and firing
The wax is removed from the dried shell. The empty ceramic shell is then fired at high temperature to obtain the mechanical and thermal strength required for metal pouring.
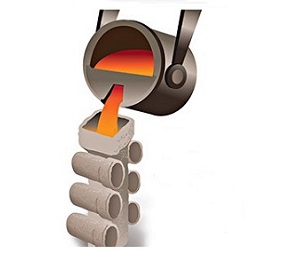
Molten metal pouring
The molten alloy is gravity-poured into the hot ceramic shell. Controlled temperatures minimise thermal shock and support uniform cooling of the casting.
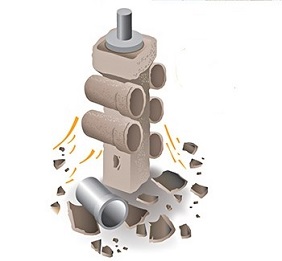
Shell removal and cut-off
After solidification, the ceramic shell is broken away. The individual castings are then separated from the central tree by mechanical or thermal cutting.
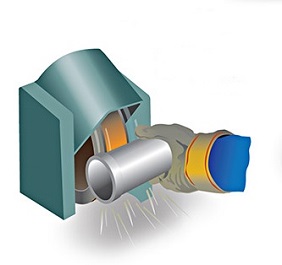
Finishing and machining
The gate areas are removed and, when required, the castings undergo heat treatment, CNC machining, drilling, threading, grinding and surface finishing.
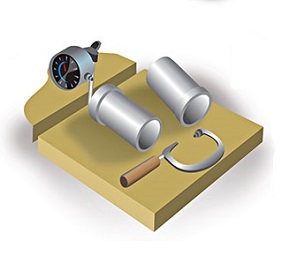
Dimensional and quality inspection
The alloy, manufacturing process and finished component are inspected to verify drawing compliance, casting integrity and consistent production quality.
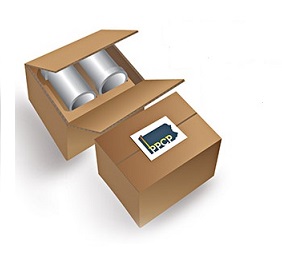
Packing, shipping and Kanban stock
Approved components are packed and shipped by sea or air. At its Parma warehouse, SR Tech manages dedicated stock and scheduled deliveries according to customised Kanban systems.
Inspection is not only the final stage
Final quality depends on systematic control of the entire cycle: wax pattern stability, shell uniformity, alloy composition, melting and pouring temperatures, cooling and subsequent operations.
- Chemical analysis of the alloy
- Dimensional inspection
- CMM inspection reports
- EN 10204 3.1 material certificate
- Visual inspection
- Specific tests on request
Learn more about investment casting
Explore the technology, view components manufactured for different industries and compare dimensional tolerances and suitable applications.
Investment casting
Technology, materials, advantages and services provided by SR Tech.
View the page → 02Investment casting products
Raw, machined and finished components for different industrial sectors.
View the products → 03Dimensional tolerances
Review achievable tolerances and the applicable dimensional tolerance grades.
View the tables → 04Technology comparison
Compare investment casting with CNC machining, forging and other processes.
Compare the processes →Would you like to know whether your component is suitable for investment casting?
Send us the 2D or 3D drawing, material specification and estimated quantities. We will evaluate the geometry, tolerances, finishing requirements and manufacturing solution.